Rail welding joins individual rails into longer strings or continuous welded rail. The main methods are flash-butt welding, aluminothermic (thermite) welding and gas-pressure welding. Flash-butt welding suits repeatable production and mobile renewal work; thermite welding suits field closures and constrained access; gas-pressure welding is used selectively where suitable equipment and procedures are available.
The welding process is only part of the job. Trimming, profile grinding, straightness checks and inspection determine whether the finished joint matches the surrounding rail and can enter service without a local impact point.
Quick comparison of rail welding methods
| Criterion | Flash-butt welding | Thermite welding | Gas-pressure welding |
|---|---|---|---|
| Joining principle | Electrical resistance heating followed by upsetting | Molten weld metal is cast into a mould around the rail gap | Gas flame heats the rail ends before pressure joins them |
| Typical location | Welding plant or mobile flash-butt welding machine | Field closure, repair, turnout or restricted-access work | Fixed or mobile specialist operation |
| Filler metal | Normally none | Thermite portion supplies weld metal | Normally none |
| Equipment footprint | High | Relatively compact | Between flash-butt and thermite systems |
| Process control | Highly mechanised and recordable | Strongly dependent on preparation and procedure control | Sensitive to heating uniformity, alignment and upsetting |
| Finishing need | Shearing or trimming followed by profile grinding | Riser removal, trimming and profile grinding | Trimming and profile finishing |
| Selection basis | Production volume, access, rail type and operator standard | Access, closure geometry, repair plan and approved procedure | Network practice, equipment availability and approved procedure |
No welding method is universally interchangeable. The infrastructure manager’s approved procedure, rail grade, joint location, access, traffic conditions and inspection requirements take priority over a general comparison.
Flash-butt rail welding
Flash-butt welding clamps two prepared rail ends in a welding head. Electrical current and controlled movement create flashing at the interface. Once the programmed heating condition is reached, the machine applies an upsetting force that expels molten material and consolidates the joint.
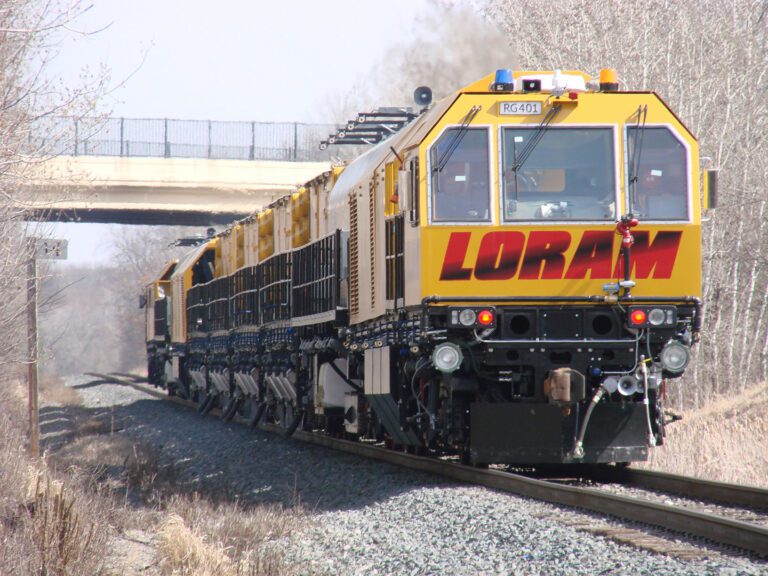
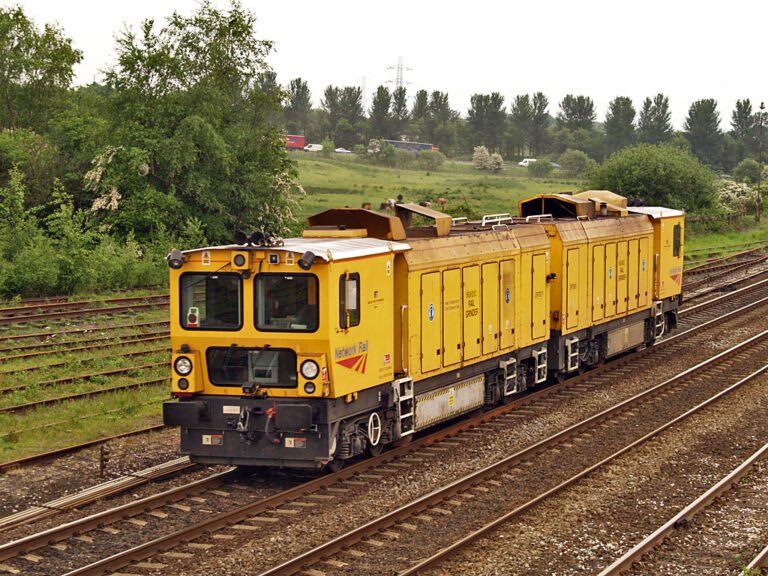
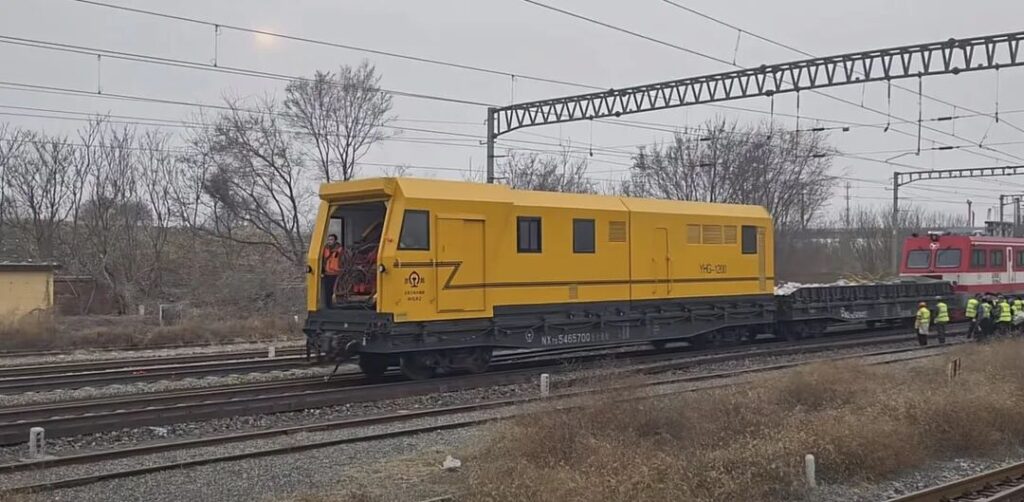
The process is used in stationary rail-welding plants and in mobile machines working on track. A fixed plant is suited to producing long rail strings under controlled conditions. A mobile flash-butt welder can make closure or renewal welds where the machine can reach and safely clamp the rail.
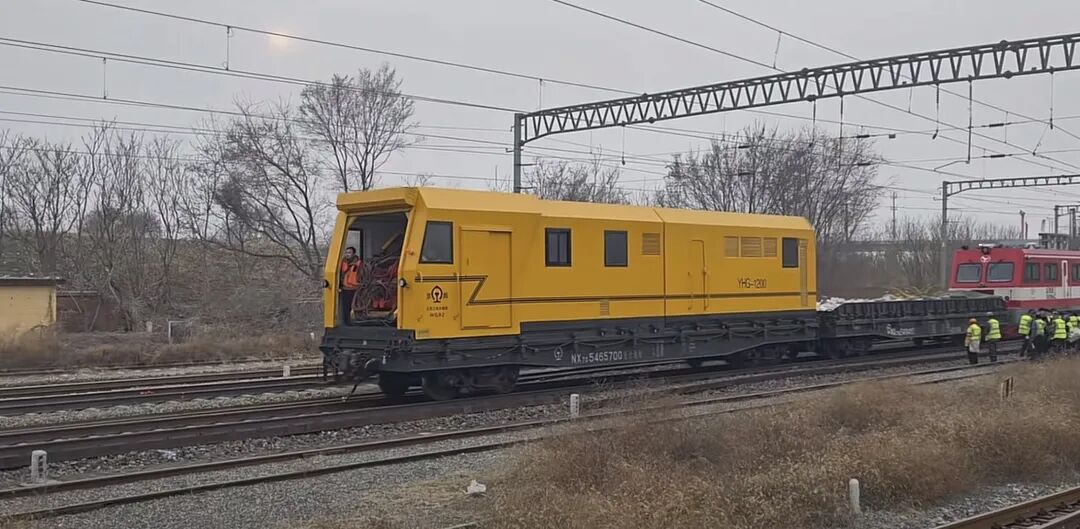
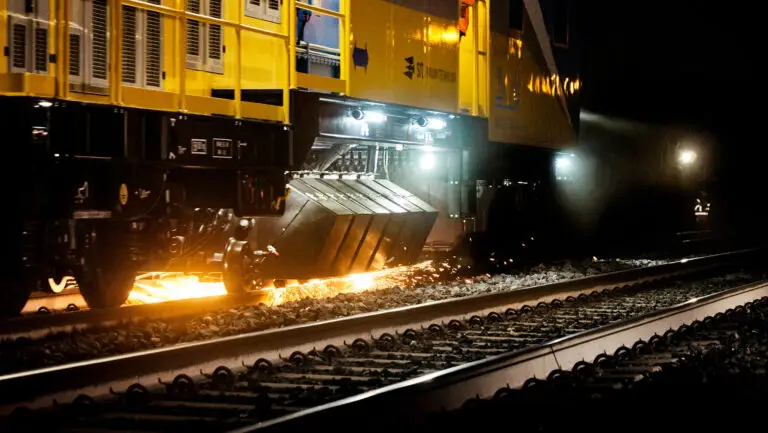
A mobile rail-welding vehicle positioned for field work.
Why operators choose flash-butt welding
- The heating, displacement and upset stages can be controlled and recorded.
- The joint is produced without adding a separate weld-metal portion.
- Mechanised trimming and profile finishing fit high-output renewal work.
- The method can be used in both fixed plants and mobile welding systems.
Its advantages come with operating constraints. The equipment needs space, power, accurate alignment and a suitable possession plan. Rail-end preparation and machine condition matter; a sophisticated welding head does not compensate for contaminated contact surfaces or poor setup.
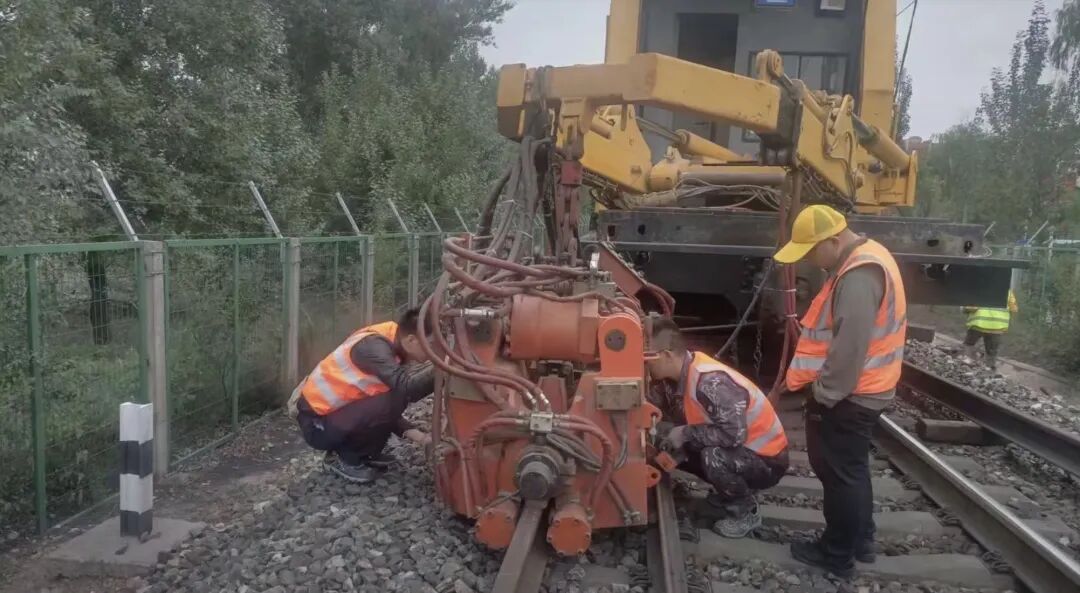
A mobile flash-butt welding head positioned at the joint.
Thermite rail welding
Thermite welding, also called aluminothermic welding, uses an exothermic reaction to produce molten steel. The rail ends are aligned with a controlled gap, enclosed by moulds and preheated. The molten metal is then poured into the mould, where it fills the gap and solidifies as the joint.
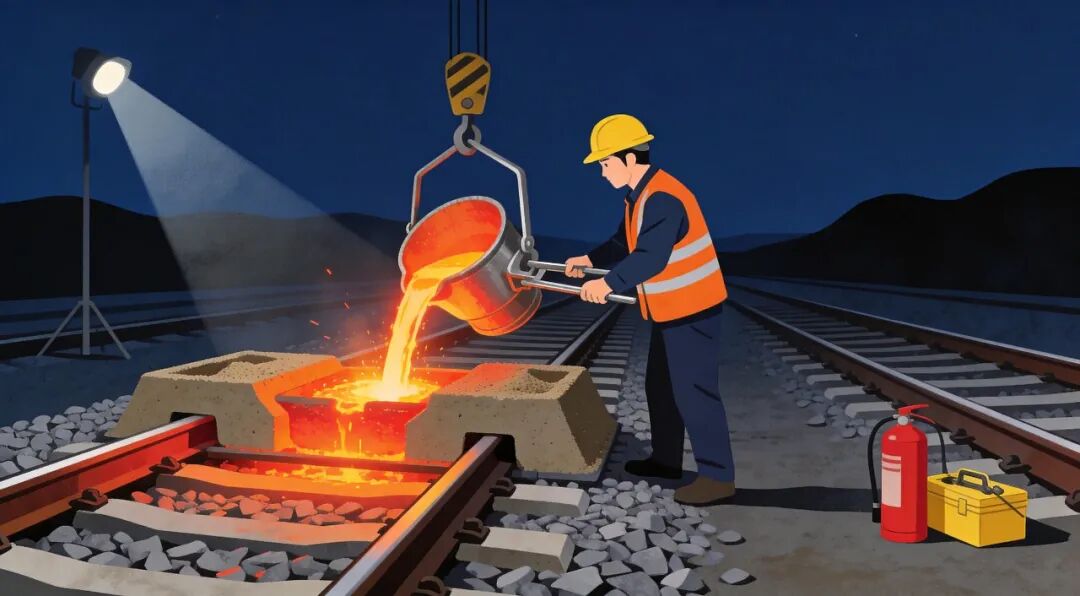
Illustration of molten weld metal being poured into a rail-joint mould.
The equipment is easier to move into restricted sites than a complete mobile flash-butt welding system. That makes thermite welding useful for approved closure welds, repairs, turnouts and locations where large rail-bound equipment cannot operate.
The trade-off is a process with many site-sensitive steps. Alignment, gap setting, mould fit, sealing, preheating, portion selection, pouring, cooling and trimming all affect the result. The exact sequence and acceptance limits must follow the railway operator’s approved welding procedure.
What happens after the pour?
Once the metal has solidified enough for the approved procedure, excess material is removed. Rough finishing must leave enough material for controlled final profiling rather than cutting into the parent rail. Final grinding then blends the running surface and gauge face into the adjacent rail.
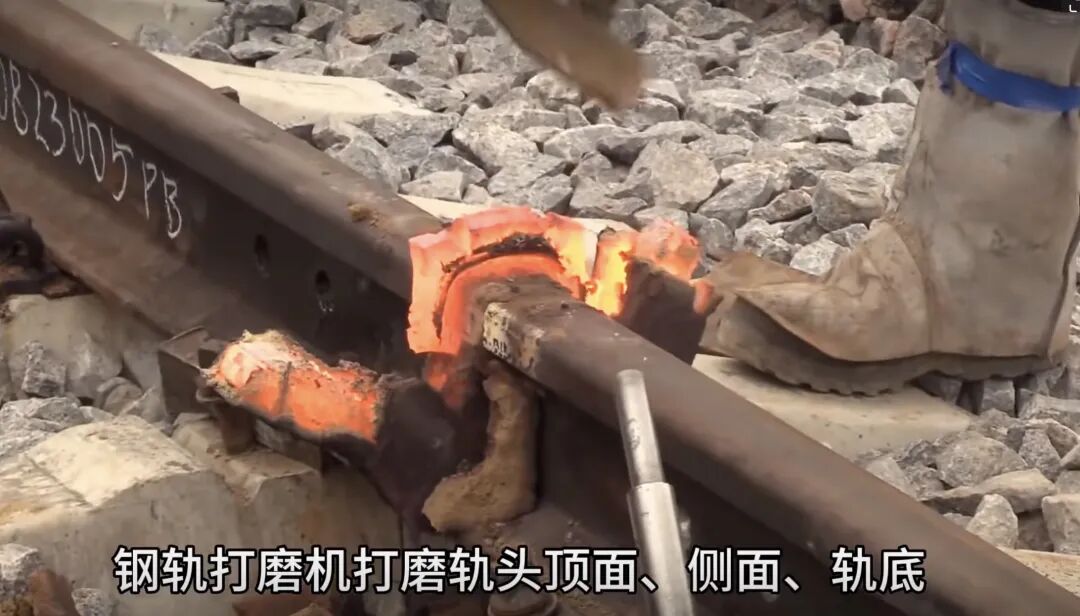
A thermite joint during post-weld finishing.
Gas-pressure rail welding
Gas-pressure welding heats aligned rail ends with a controlled gas flame while axial force is applied. The ends are joined in the plastic state rather than by pouring filler metal into a mould. Fixed and mobile systems exist, but adoption varies by network and region.
The method can produce a pressure-forged joint with a smaller equipment footprint than some flash-butt systems. Its control challenges include heating uniformity, weather exposure, rail-end alignment and repeatable upsetting. It should therefore be described as a specialist option, not a universal middle ground between flash-butt and thermite welding.
Flash-butt vs thermite welding: which should be used?
Choose the method through an approved engineering decision, not a simple ranking.
Production and repeatability
Flash-butt welding generally fits high-volume work where a fixed plant or mobile welding machine can be deployed. Its mechanised cycle provides process records that support quality control.
Thermite welding is assembled and executed at the joint. It is valuable where access or closure geometry makes large equipment impractical, but each preparation step must be controlled in the field.
Access and possession planning
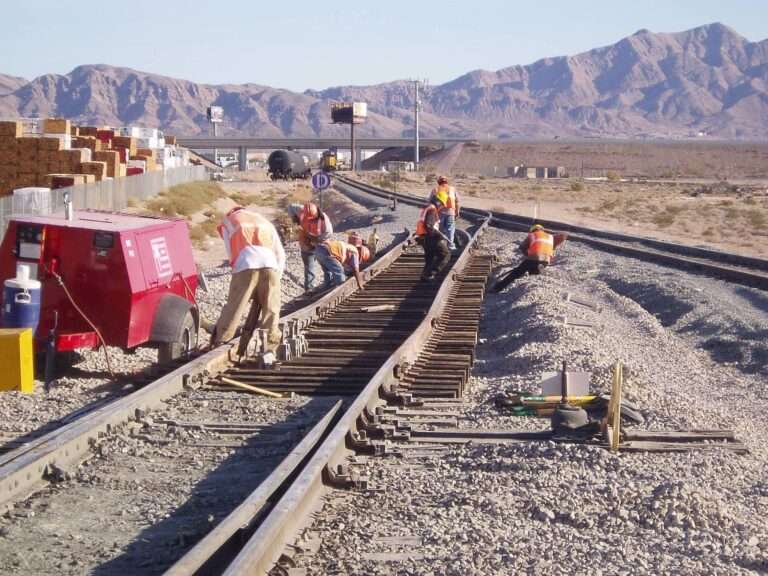
A mobile flash-butt machine needs track access, room for the welding head and a possession plan that accommodates the machine. Thermite equipment can be carried to more constrained locations, including complex trackwork, subject to the operator’s approval.
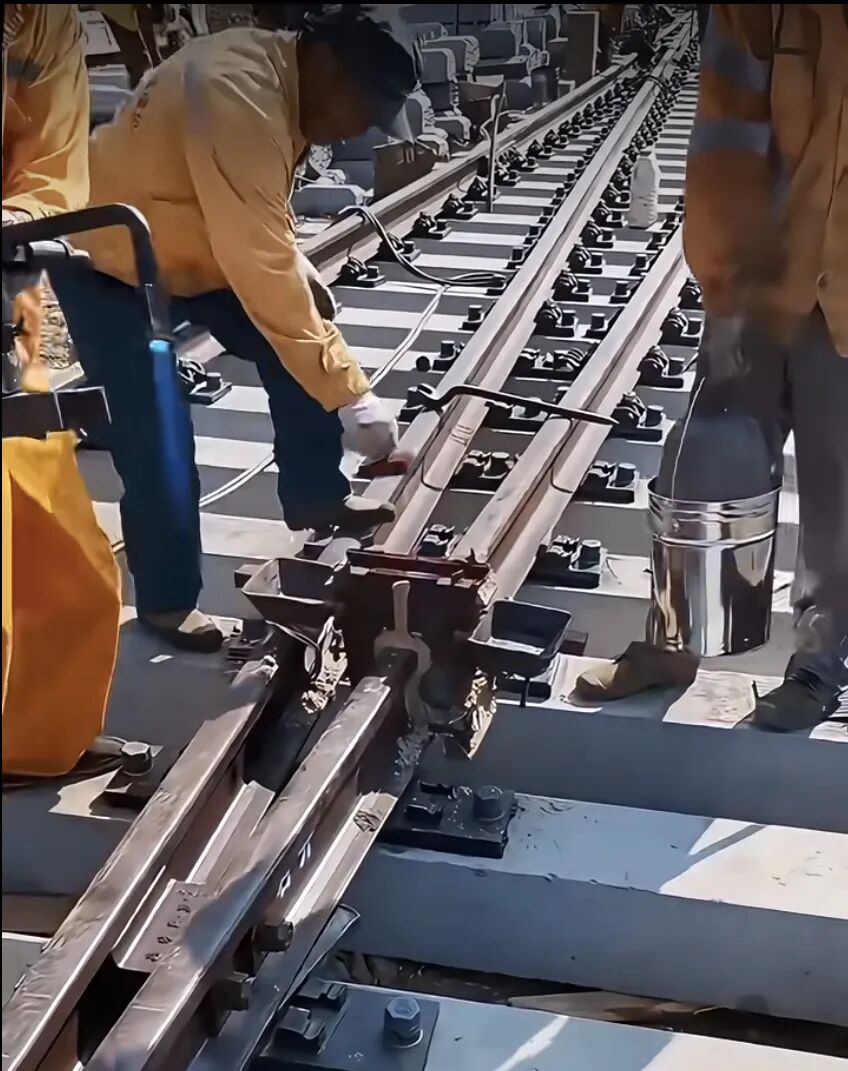
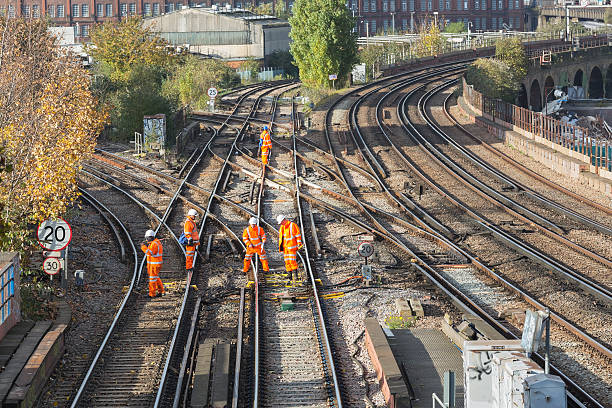
Field welding at a constrained track location.
Joint finishing
Both processes require finishing. Flash-butt welding leaves upset material that is sheared or trimmed before grinding. Thermite welding leaves a cast riser and local excess material that must be removed before the final profile is restored.
The finishing load is not identical, but the objective is: a smooth transition through the weld with no damaging notch, burn or local profile error.
Why rail weld grinding matters
Rail weld grinding restores the rail-head profile after trimming. It is not cosmetic polishing. A joint that is high, low, faceted or thermally damaged can create impact loading, noise, accelerated local wear and an inspection failure.
The RDSO flash-butt welding manual requires the rail-head surfaces to be ground flush with the parent rail and specifically warns against grinding burns and notches. It also describes staged profile grinding for in-situ flash-butt welds. Requirements differ between networks, so the applicable operator standard remains the controlling document.
A practical finishing sequence
- Remove the upset or riser using the approved trimming method.
- Allow the joint to reach the temperature range specified by the welding procedure.
- Rough-grind the excess without cutting into the parent rail.
- Profile the rail head and gauge corner with controlled passes.
- Check longitudinal straightness and transverse profile using approved gauges.
- Inspect for surface damage, grinding burn and remaining discontinuities.
- Complete the required non-destructive examination and joint marking.
Grinding pressure, contact time and wheel condition must be controlled. Holding an abrasive wheel in one place can overheat the rail. Chasing a low spot by grinding the surrounding parent rail can turn a local finishing error into a longer geometry defect.
Selecting an abrasive wheel for weld finishing
Machine model alone does not confirm wheel compatibility. Before ordering a profile grinding wheel, record:
- Grinder manufacturer and exact model
- Wheel outside diameter, thickness and bore or thread
- Mounting interface and flange arrangement
- Maximum permitted wheel and spindle speed
- Rail grade and weld type
- Rough-grinding or finish-profiling duty
- Benötigte Menge und Bestimmungsland
For available configurations, see our Sortiment an Profilschleifscheiben. For wider maintenance context, read Normen und praktische Verfahren für das Schleifen von Schienen und Grinding Burn on Rails.
If the weld is made with a mobile flash-butt system, the equipment overview for the Plasser & Theurer APT 1500 R provides a useful example of an integrated rail-welding workflow.
Common rail-welding and finishing mistakes
Treating every weld location the same
Mainline renewal, a closure weld, a turnout and an emergency repair impose different access and acceptance conditions. The approved network procedure must be checked before choosing the process.
Grinding before the joint is ready
Temperature windows and trimming stages differ between procedures. Grinding too early or too late can affect surface condition and the amount of material left for final profiling.
Using a wheel because its diameter looks correct
Diameter is only one compatibility field. The mounting, thread or bore, speed rating, thickness and grinder configuration must all match.
Removing parent rail to hide a profile error
Final grinding should blend the weld into the rail. It should not create a long hollow around the joint. Measure after each controlled stage rather than relying on visual appearance.
Häufig gestellte Fragen
What are the main types of rail welding?
The main methods are flash-butt welding, aluminothermic or thermite welding, and gas-pressure welding. Some networks also use enclosed-arc or other specialist repair-welding processes. The permitted method depends on the rail, location and infrastructure manager’s procedure.
Is flash-butt welding stronger than thermite welding?
They form joints through different metallurgical routes and are controlled by different procedures. Flash-butt welding is a pressure-forging process without separately poured filler metal; thermite welding creates a cast weld. Do not apply a universal strength percentage without the rail grade, procedure and test standard.
Does a flash-butt weld need grinding?
Yes. After upsetting, excess material is removed and the joint is finish-ground so the rail-head surfaces blend with the parent rail. Grinding must avoid burns, notches and profile damage.
Why is thermite welding still used?
Thermite equipment can be taken to locations that are difficult for a rail-bound welding machine to reach. It remains useful for approved field closures, repairs and constrained trackwork where the operator’s procedure permits it.
Can the same grinding wheel be used on every rail weld?
No. Confirm the grinder, dimensions, mounting system, speed rating, rail material and whether the job is rough removal or final profiling. Similar-looking wheels are not automatically interchangeable.
Technical references
- RDSO Manual for Flash Butt Welding of Rails
- JFE Steel: Rail Flash-Butt Welding Technology
- Nippon Steel technical report on rail welding
- Korea National Railway: How rail welded joints are constructed
Request wheel compatibility confirmation
Send the grinder manufacturer and model, wheel dimensions and marking, mounting details, weld type, required quantity, destination country and delivery date. Our technical team can review the information and recommend a suitable rail profile grinding wheel configuration.